Personal protective equipment is an essential part of many workplace safety programs, but managing that equipment can become surprisingly complicated as an organization grows.

Gloves, safety glasses, respirators, hearing protection, protective clothing, and other products may be distributed across multiple departments, shifts, facilities, or job roles. When purchasing and distribution are handled through open supply closets, spreadsheets, manual requests, and disconnected vendors, employers can lose visibility into how much equipment is being used, where shortages are developing, and whether workers are receiving the correct approved products.

Those gaps can create both financial and safety problems. Facilities may overstock products that employees rarely use while running out of high-demand items. Workers may take more PPE than necessary because there is no meaningful inventory control. Different locations may buy different products for the same task, making standardization and training more difficult.

Managed PPE programs provide a more structured approach by combining approved product selection, inventory management, point-of-use distribution, usage tracking, replenishment, and ongoing program oversight. When designed around a workplace hazard assessment, the result can give employees easier access to the equipment they need while helping employers reduce unnecessary consumption and maintain more consistent PPE practices.

What Is a Managed PPE Program?

A managed PPE program is a structured system for controlling how protective equipment is selected, stocked, distributed, replenished, and tracked across a workplace or organization. Instead of treating PPE primarily as individual purchase orders, the employer establishes an approved program around the products employees actually need for their assigned hazards and tasks.

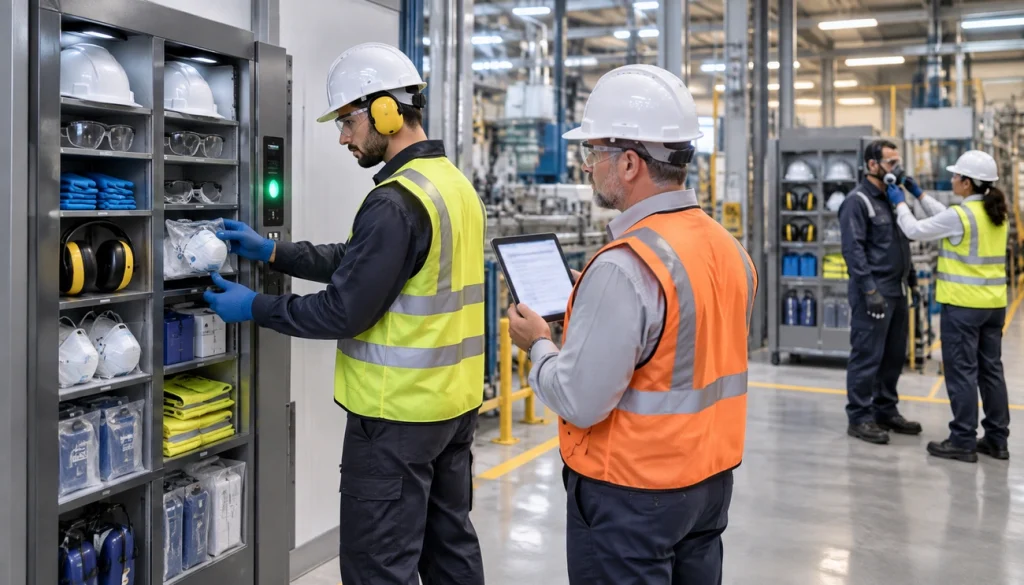
The exact model can vary. Some organizations use PPE vending machines at the point of use, while others combine vending with lockers, central inventory, specialty programs, reporting, and supplier-managed replenishment. Multi-site employers may also standardize approved products so similar operations use consistent equipment across facilities.

Managed PPE Is More Than Automatic Dispensing

A vending machine is one useful component, but the broader program should begin with safety requirements rather than hardware. Employers still need to determine which equipment employees need, which models are approved, where different sizes are required, and how often reusable equipment must be inspected or maintained.

Once those decisions are established, managed distribution can make the program easier to operate. The system controls which products are available, where they are located, and how employees access replacements during the workday.

This distinction is important because reducing PPE cost should never mean limiting employees’ access to protection they are required to use.

Traditional PPE Purchasing Can Hide Usage Problems

In a traditional supply-room model, supervisors may order several cases of gloves, glasses, or respirators and distribute them as employees request replacements. Unless someone records every transaction, the organization may know what it purchased without knowing where the products went.

That makes several questions difficult to answer. Is one department using twice as many gloves because the task damages them quickly? Are employees taking extra items to keep in personal lockers? Is one facility purchasing a different product for the same hazard? Are shortages occurring because inventory levels are too low or because equipment is being used inefficiently?

A managed system creates better visibility into these patterns.

How PPE Vending Changes Distribution

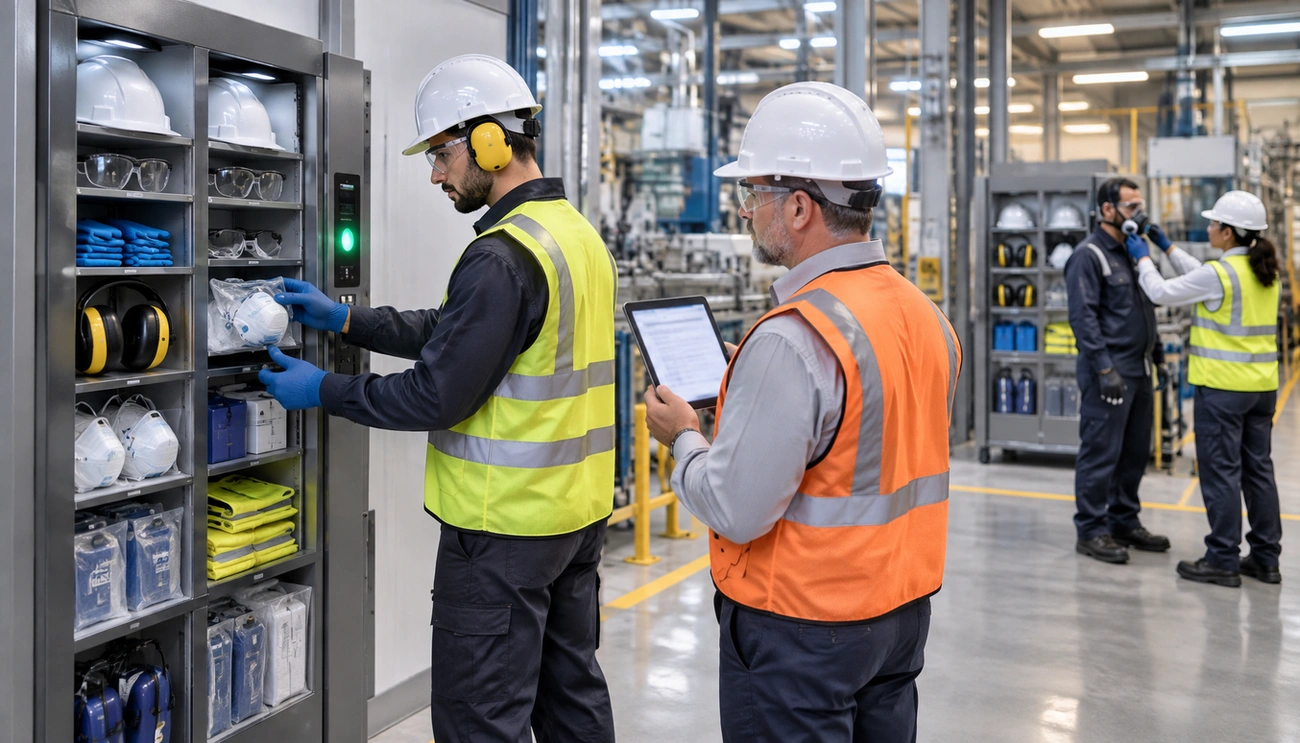
PPE vending moves commonly used safety products closer to the people who need them while adding controls around access and inventory.

Arbill’s PPE Vending Program combines vending machines, lockers, collection options, real-time usage reporting, configurable dispensing controls, and inventory monitoring. Arbill’s current system also allows employers to configure specific products or dispensing limits by employee or division while monitoring inventory and vending patterns.

The goal is not simply automation. It is creating a more predictable PPE supply process.

Point-of-Use Access Can Reduce Delays

Employees should not need to search for a supervisor every time a pair of gloves becomes damaged or safety glasses need replacement. If PPE is difficult to access, employees may delay work, leave their area to find supplies, or in a poorly managed environment, continue without suitable protection.

Placing approved PPE near the work area can reduce that friction. This can be particularly useful for facilities operating several shifts because workers maintain access even when purchasing personnel or storeroom staff are unavailable.

Point-of-use availability also allows damaged or contaminated disposable equipment to be replaced promptly without creating unnecessary administrative steps.

Controlled Dispensing Improves Accountability

Open cabinets make it difficult to know how much equipment individual departments or employees are using. Controlled dispensing provides more visibility while still keeping necessary equipment available.

The purpose should not be to penalize workers for replacing damaged PPE. Instead, usage data can help safety teams identify unusual patterns that deserve investigation.

If one operation consumes significantly more cut-resistant gloves than similar departments, for example, the employer can ask whether the selected glove is appropriate for the material being handled. High usage could indicate excessive wear, a poor product match, improper use, or simply a more demanding task.

The data creates a question worth investigating rather than automatically treating consumption as waste.

Managed PPE Programs Can Reduce Excess Inventory

One of the clearest opportunities for cost control is reducing unnecessary stock.

Organizations frequently keep large quantities of safety products in storage because they do not have reliable information about actual consumption. Managers may reorder early to avoid shortages, while another department already has several unopened cases of the same item.

A managed system can provide a more accurate picture of what employees use and how quickly inventory moves.

Better Usage Data Supports Better Reordering

When usage patterns are visible, inventory levels can be based on actual consumption rather than estimates.

Frequently used products can receive higher stocking levels, while slow-moving products can be managed more conservatively. This reduces the chance that capital remains tied up in excessive stock or that products become obsolete before they are used.

Real-time inventory monitoring can also help identify shortages earlier, giving the organization time to replenish critical PPE rather than discovering that the supply cabinet is empty during a shift.

Standardization Reduces Unnecessary Product Variation

Large organizations often accumulate multiple versions of similar PPE over time.

One facility may purchase one cut-resistant glove while another orders three alternatives. Different supervisors may select different safety glasses, earplugs, or disposable respirators even when employees perform comparable work.

Standardization can reduce this complexity.

Once the employer has evaluated the hazards and approved products for specific tasks, purchasing can concentrate on a smaller, defined selection. This can simplify ordering, training, inventory management, and replacement while giving the organization clearer visibility into overall PPE consumption.

Arbill’s guide to PPE program management for multi-site industrial operations explains how standardized selection and inventory control can help organizations manage protective equipment more consistently across locations.
Explore Our Solutions!
How Managed Personal Protective Equipment Programs Cut Costs While Keeping You Compliant

Managed PPE Can Reduce Product Waste

Waste does not come only from purchasing too much inventory. It can also occur at the point of use.

Employees may take several items at once because supplies are inconvenient to reach or because they are uncertain whether replacements will be available later. Open supply areas may also make products easy to remove for tasks where they are not required.

A managed program can reduce these behaviors without restricting legitimate safety needs.

Dispensing Limits Can Control Routine Consumption

Where appropriate, configurable dispensing limits can establish reasonable access based on job role or department.

These controls should be designed carefully. A worker who damages required PPE must still be able to obtain a safe replacement.

For that reason, managed PPE should include an exception process rather than treating every replacement beyond a predefined limit as misuse.

The objective is accountability, not rationing.

Usage Trends Can Reveal Product-Selection Problems

High consumption may also signal that the equipment itself is not appropriate.

If a glove repeatedly fails halfway through a shift, increasing restrictions on glove access does not solve the real problem. The organization should evaluate whether a different glove material, coating, construction, or performance level is better suited to the task.

This is one reason managed PPE data should be reviewed by safety professionals rather than used solely by purchasing.

Cost control and hazard protection need to remain connected.

Reduce Administrative Time Spent Managing PPE

PPE has costs beyond the price printed on a purchase order.

Employees spend time checking stock, submitting requests, receiving deliveries, distributing equipment, counting inventory, and tracking shortages. Supervisors may also spend time searching for replacements or approving routine PPE requests.

When those activities occur manually across many departments, the administrative cost can become significant.

Automated Inventory Monitoring Reduces Manual Counts

Usage reporting and inventory monitoring can reduce the need for repeated manual stock checks. Safety and purchasing teams can review current inventory and consumption trends rather than physically counting every cabinet on a fixed schedule.

This allows staff to spend more time investigating safety issues and less time performing basic inventory administration.

Point-of-Use Distribution Reduces Internal Handling

Central supply rooms often require someone to receive, store, issue, and transport products to departments. Point-of-use systems shorten that distribution chain.

Employees obtain approved PPE closer to where it will be used, which can reduce travel time and simplify replacement during a shift.

For large facilities or multiple operating areas, those small time savings can accumulate across hundreds of routine PPE transactions.

Cost Reduction Should Never Override Hazard Assessment

Managed PPE programs can improve efficiency, but cost should never determine protection before the hazard does.

OSHA’s general PPE requirements require employers to assess the workplace, determine whether hazards are present or likely to be present, and select PPE that protects employees from those identified hazards. The standard also requires the selected PPE to properly fit each affected employee. (OSHA 1910.132)

That responsibility remains with the employer regardless of who manages the inventory.

Select PPE Before Configuring Distribution

Before stocking vending machines or establishing standardized product lists, employers should know which PPE is appropriate for each task.

The process should consider the hazard, exposure route, required performance, employee fit, compatibility with other equipment, and manufacturer limitations.

Arbill’s guide on how to choose workplace safety equipment for employees provides a broader framework for connecting hazard assessment with PPE selection, worker trials, fit, training, and maintenance.

Avoid Standardizing the Wrong Product

Standardization creates savings only when the standardized item is appropriate.

Using one glove across an entire organization may simplify purchasing, but it may leave workers inadequately protected if different operations involve cuts, heat, chemicals, puncture hazards, or other exposures.

The correct approach is to standardize where the hazard and performance requirements are comparable while maintaining specialized PPE where the work requires it.

How Managed PPE Programs Support Compliance

PPE compliance involves much more than proving that equipment was purchased.

Employers need appropriate hazard assessments, product selection, employee training, proper use, fit, maintenance, and replacement processes. Certain PPE categories, particularly respiratory protection, also have additional program requirements.

Managed distribution can support these responsibilities by improving availability, standardization, tracking, and visibility, but it does not replace them.

Better Access Supports Consistent PPE Use

Employees are more likely to use required PPE consistently when approved equipment is readily available.

If safety glasses are repeatedly unavailable on night shift or workers cannot replace damaged gloves without finding a supervisor, the distribution system creates unnecessary barriers to compliance.

Point-of-use access can help remove these barriers while ensuring workers select from products the safety team has already approved.

Product Controls Help Prevent Unapproved Substitution

When approved equipment is unavailable, workers or supervisors may substitute whatever product they can find.

That substitute may look similar without having the same performance rating, chemical resistance, fit, or compatibility.

A managed PPE system helps maintain an approved product list and makes those products consistently accessible, reducing the likelihood of informal substitutions.

PPE Distribution Records Support Program Oversight

Usage records can provide useful information about who accessed certain products and when.

These records may help safety teams investigate consumption patterns, confirm that products are available across shifts, or evaluate whether a new PPE requirement is actually being implemented.

However, distribution records should not be confused with proof that an employee used the equipment correctly.

Issuing PPE Does Not Prove Compliance

A vending record showing that an employee received safety glasses does not show that they wore them throughout the exposure.

A record showing that a respirator was dispensed does not demonstrate that the respirator was properly selected, medically approved, fit tested, or used correctly.

Managed PPE data should therefore support inspections, training, observations, and other safety-program activities rather than replacing them.

Respiratory Protection Requires Additional Controls

Respiratory PPE deserves particular attention because selecting and distributing a respirator is only one part of a compliant program.

OSHA’s respiratory protection standard requires covered employers to evaluate respiratory hazards, select appropriate respirators, provide medical evaluations and required fit testing, train employees, maintain respirators properly, and periodically evaluate the program.

A managed inventory system can make approved respiratory equipment easier to access, but it cannot substitute for these program elements.

Respirator Selection Must Match the Hazard

Different respiratory hazards require different protection.

Disposable filtering facepiece respirators, reusable air-purifying respirators, powered air-purifying respirators, supplied-air systems, and self-contained breathing apparatus serve different purposes and have different limitations.

Arbill’s Respiratory Protection offering includes categories such as disposable respirators, reusable respirators and cartridges, PAPRs, supplied-air equipment, SCBA, fit-testing products, storage products, and cleaning supplies.

The presence of these options reinforces why respiratory protection should be selected according to the exposure rather than simply choosing the most convenient product to stock.

Fit Testing Remains Essential

Where OSHA requires the use of a tight-fitting respirator, fit testing is part of the respiratory protection program. An employee may be issued the correct model yet receive inadequate protection if the facepiece does not seal properly.

Managed PPE can help standardize which respirator models are available and keep replacement components stocked, but fit testing and medical evaluation remain separate employer responsibilities.

Cleaning and Storage Matter

Reusable respiratory equipment needs appropriate inspection, cleaning, maintenance, and storage.

A managed PPE program can make compatible cleaning products, filters, cartridges, replacement parts, and storage solutions easier to control, but the organization still needs procedures that define when and how these activities occur.

”As long as people go to work, we have an opportunity to help protect them.

Julie Copeland
Arbill CEO

Julie Copeland Arbill CEO

Employer-Paid PPE Requirements Still Apply

Most PPE required to comply with OSHA standards must be provided by the employer at no cost to employees, subject to limited exceptions in the standard. OSHA specifically notes that many commonly required items fall under this employer-payment obligation.

A managed program can make this responsibility easier to administer because approved equipment is distributed through a defined system rather than through individual employee purchases or informal reimbursement.

The organization should still review the actual OSHA requirements that apply to each PPE category rather than assuming every item follows identical payment rules.

Managed PPE Can Improve Multi-Site Consistency

PPE management becomes significantly more complicated when an organization operates several facilities.

Different sites may have similar hazards but different product lists, suppliers, purchasing procedures, and replacement practices. Over time, this can create inconsistent protection and fragmented spending.

A managed program provides an opportunity to establish common standards while still allowing exceptions where site-specific hazards require them.

Standardize Comparable Tasks

If several facilities perform the same operation under comparable conditions, they may be able to use the same approved PPE.

This can simplify procurement, training, product documentation, and inventory management.

Preserve Site-Specific Requirements

Standardization should not override local hazard assessments.

One manufacturing site may handle chemicals another location never uses. Another may have higher noise exposure or different electrical hazards.

The corporate PPE program should create consistency where appropriate while allowing specialized equipment when the risk requires it.

Usage Data Can Strengthen Safety Decisions

One of the most valuable features of managed PPE is that distribution becomes measurable.

Instead of asking only how much the company spent, safety teams can examine where the equipment is being used.

High Consumption Can Reveal Hidden Problems

An unusual increase in glove usage may indicate product failure, a process change, or inappropriate selection.

A sudden rise in eye-protection replacement could indicate that eyewear is being damaged because storage is poor.

Increased respiratory filter usage may reflect longer task duration, changed exposure conditions, or an operational change that deserves investigation.

The data does not automatically explain the problem, but it can show where safety teams should ask additional questions.

Low Usage Can Also Be Important

Low consumption is not always positive.

If a department is expected to use hearing protection but rarely accesses replacement plugs or earmuffs, the safety team may need to determine whether employees already have adequate supplies or whether required protection is not being used consistently.

PPE data becomes more useful when it is compared with hazard assessments, employee observations, inspection findings, and incident information.

Arbill’s article on how smart PPE is changing workplace safety discusses how connected distribution and other safety technologies can give employers more visibility into workplace protection.

Managed Programs Can Support Sustainability Goals

Inventory control can also reduce material and packaging waste.

Ordering excessive quantities increases the risk that products become obsolete or remain unused. Uncontrolled dispensing can create unnecessary disposal, while individually packaged distribution can generate additional packaging.

Arbill’s current vending system is designed around configurable cells, reduced packaging, inventory monitoring, and collection options for used items. The company positions these features as supporting waste reduction and broader sustainability goals.

Sustainability should still remain secondary to protection. PPE should never be reused, retained, or replaced less frequently simply to reduce waste when its condition requires removal from service.

How to Choose a Managed PPE Provider

Selecting a provider involves more than comparing product catalogs.

A strong program should support the organization’s approved PPE strategy, inventory needs, workforce, facility layout, and reporting requirements.

Evaluate Product and Technical Support

The provider should be able to supply the approved products, sizes, and accessories required by the workplace.

Ask what happens if a product is discontinued or temporarily unavailable. Substitutions should be reviewed against the employer’s hazard assessment rather than automatically replacing the approved model with something that appears similar.

Technical support can also be important for specialized categories such as respiratory protection, chemical-resistant gloves, fall protection, and head protection.

Review Vending and Locker Capabilities

The physical distribution system needs to fit the work environment.

Consider where employees need PPE, which items are used frequently, whether equipment needs charging or return tracking, and how many workers use each location.

Arbill’s current system includes high-capacity drum vending machines as well as lockers that can support returns, damaged-item status, and optional internal charging.

The right setup depends on the workplace rather than simply selecting the largest machine available.

Understand Reporting Capabilities

Before implementation, determine which information the organization actually needs.

Useful reporting may include consumption by:

Employee, department, facility, product, or time period.

Safety teams should also determine who will review the information and what actions should occur when unusual trends appear.

Collecting data that nobody analyzes adds administrative complexity without improving safety or cost control.

Evaluate Maintenance and Restocking Support

A vending program becomes ineffective when equipment remains offline or high-use PPE is continually out of stock.

Clarify:

Who monitors inventory, who restocks the equipment, how maintenance issues are reported, and what support is available if a unit fails.

Arbill states that its PPE vending program includes real-time inventory monitoring along with maintenance and product support for its machines.

Pilot the Program Before Expanding

Organizations with multiple departments or facilities may benefit from beginning with a controlled pilot.

Choose an area with meaningful PPE consumption and a clear baseline of current costs and usage.

The pilot can reveal practical problems before a larger rollout.

Establish a Baseline

Before implementation, document current:

PPE spending, product usage, stockouts, inventory levels, ordering time, and waste where those figures are available.

Without a baseline, it becomes difficult to determine whether the managed program actually improved performance.

Include Employees in the Pilot

Workers should be able to explain whether the new distribution system is convenient and whether the approved products remain appropriate for their work.

If employees routinely bypass the machine because the correct size is unavailable or the equipment is located too far away, the program needs adjustment before expansion.

Review Safety and Cost Results Together

A successful pilot should not be judged only by lower spending.

Evaluate whether PPE remained accessible, whether stockouts declined, whether approved products were used consistently, and whether employees experienced any problems obtaining replacements.

Cost reduction is valuable only when protection remains appropriate.

See Our Safety Services!
PPE Products

Measure Savings Carefully

Managed PPE programs can reduce waste and administrative burden, but employers should avoid assuming a fixed savings percentage before reviewing their own data.

Savings depend on existing purchasing practices, workforce size, product standardization, previous overstocking, consumption patterns, and the degree of administrative work being replaced.

Compare Total Program Cost

Include more than product prices.

Consider:

Vending or service costs, inventory, administration, maintenance, employee time, obsolete stock, emergency purchases, and other relevant expenses.

Then compare those costs with the previous distribution model.

Verify the Source of Savings

If glove spending falls, determine why.

Did employees stop over-dispensing? Was a better-performing glove selected? Did purchasing negotiate a better price? Did the organization accidentally restrict necessary access?

Understanding the reason ensures that savings reflect improvement rather than a new safety problem.

Common Managed PPE Program Mistakes

A managed program can become ineffective when organizations focus on the distribution technology without maintaining the safety program behind it.

One common mistake is stocking vending machines before completing an adequate hazard assessment. The machine may efficiently dispense equipment that is not actually appropriate for the task.

Another mistake is setting aggressive dispensing restrictions based primarily on cost. Required PPE needs to remain available whenever it becomes damaged, contaminated, lost, or otherwise unsuitable for continued use.

Organizations can also collect extensive usage data without assigning anyone to review it. The value of the system comes from acting on unusual patterns, not simply producing reports.

Finally, employers should not assume that vendor management transfers their regulatory responsibilities. Hazard assessment, product selection, training, fit, proper use, and specialized PPE-program requirements remain employer obligations.

A Practical Managed PPE Program Checklist

Before expanding a managed PPE program, businesses should confirm that:

  • Workplace hazard assessments identify which PPE each task requires.
  • Approved products and acceptable substitutes are documented.
  • Required sizes and configurations are available.
  • PPE remains accessible across relevant shifts and work areas.
  • Dispensing controls do not prevent legitimate replacement.
  • Usage reports are reviewed for unusual consumption patterns.
  • Inventory levels are monitored to prevent stockouts.
  • Employees receive required PPE training.
  • Respiratory-protection requirements are managed separately where applicable.
  • Reusable equipment has inspection, cleaning, and storage procedures.
  • Responsibilities for restocking and vending maintenance are clear.
  • Cost savings are compared with a documented baseline.
  • Safety performance is reviewed alongside financial results.

The goal is a program that improves both efficiency and protection rather than optimizing one at the expense of the other.

Conclusion

Managed PPE programs can help businesses gain better control over one of the most recurring parts of workplace safety spending.

By combining standardized approved products, point-of-use access, controlled dispensing, real-time inventory visibility, usage reporting, and structured replenishment, employers can reduce many of the inefficiencies associated with open supply closets and disconnected purchasing systems.

Those improvements can lead to lower excess inventory, less unnecessary consumption, fewer emergency orders, reduced administrative work, and better visibility into how PPE is being used across departments and facilities.

The compliance benefit is equally important. Employees are more likely to have consistent access to approved PPE, while safety teams gain information that can help identify stockouts, unusual consumption, product problems, or gaps in implementation.

However, a managed PPE program does not replace the employer’s underlying safety responsibilities. Employers still need to assess hazards, select appropriate equipment, ensure proper fit, train employees, inspect and maintain reusable PPE, and meet specialized requirements such as respiratory medical evaluations and fit testing.

The strongest programs therefore combine logistics with safety management.

The provider helps make approved protection available and measurable. The employer continues to determine what protection employees need and whether the overall program works.

When those responsibilities are aligned, managed PPE can do more than simplify purchasing. It can help businesses control costs, maintain more consistent PPE practices, and build a stronger foundation for workplace compliance.

Request a Safety Assessment

Recent Posts

How to Conduct a Risk Assessment That Actually Prevents Workplace Injuries
How to Identify Workplace Hazards Before They Lead to Injuries

How to Identify Workplace Hazards Before They Lead to Injuries

How Managed Personal Protective Equipment Programs Cut Costs While Keeping You Compliant
How Managed PPE Programs Help Businesses Reduce Costs and Improve Compliance

How Managed PPE Programs Help Businesses Reduce Costs and Improve Compliance

How to Build an Effective Workplace Safety Program for Your Business

How to Build an Effective Workplace Safety Program for Your Business

Workplace Safety Training Requirements Every Employer Must Follow
Workplace Safety Training Requirements: What Employers Need to Know

Workplace Safety Training Requirements: What Employers Need to Know

Risk Assessment for Environmental Health and Safety
Environmental Health and Safety Assessments: What Businesses Need to Know

Environmental Health and Safety Assessments: What Businesses Need to Know

  • Previous ProjectHow to Identify Workplace Hazards Before They Lead to Injuries

  • Next ProjectHow to Build an Effective Workplace Safety Program for Your Business

CUSTOMER SERVICE

800-523-5367

CONTACT US

Complete the short form below and an Arbill representative will get back to you within 24 hours.
* Required Fields

    ARBILL RESPECTS YOUR PRIVACY AND YOUR INFORMATION: By submitting the form above you agree to receiving emails from Arbill. Your submitted information is NEVER shared. You may unsubscribe at any time via the "unsubscribe" link in our emails. You can view our Privacy Policy HERE.